High Hardness RTV-2 Platinum Cure Liquid Silicone Rubber

high hardness odor freenon toxic 40-50 A platinum based low shrinkage
  • Pricing: Custom Quote
  • HS Code: 3910.00.0000
  • MOQ: 2 kg Kit (1 kg Part A + 1 kg Part B)
Estimated Lead Time
  • 2-3 Days
    < 1,000 Kg
  • 4-7 Days
    1-5 Tons
  • Negotiable
    > 5 Tons

See real testimonials from customers who have used our products.

1. Description

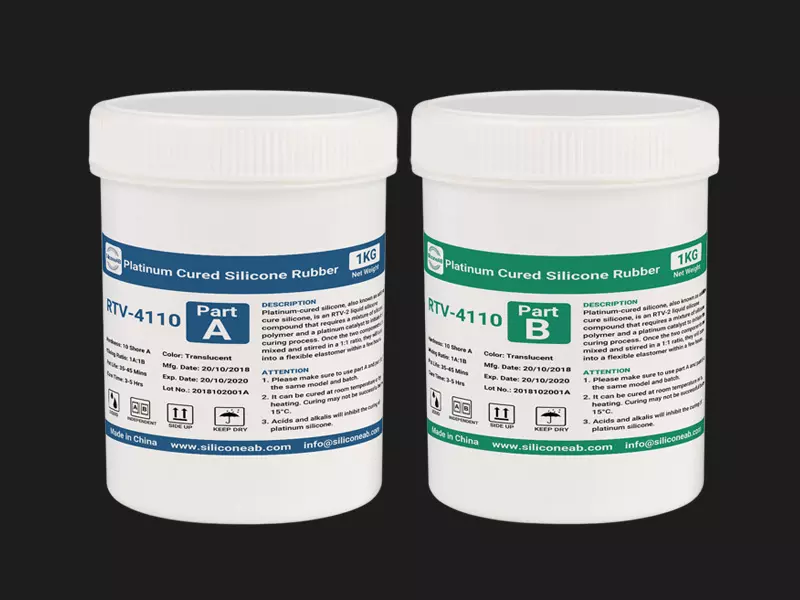
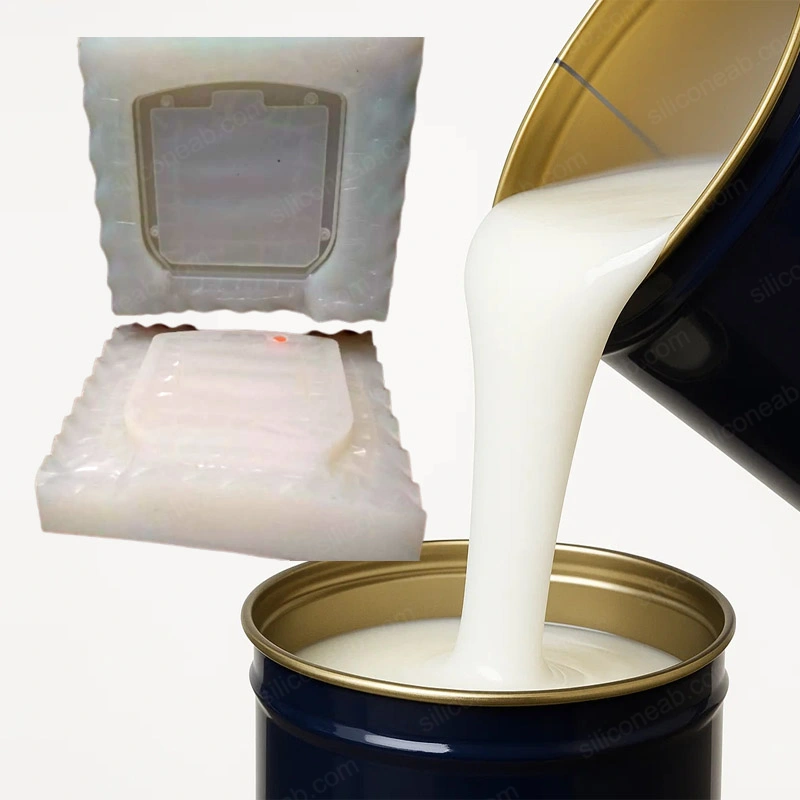
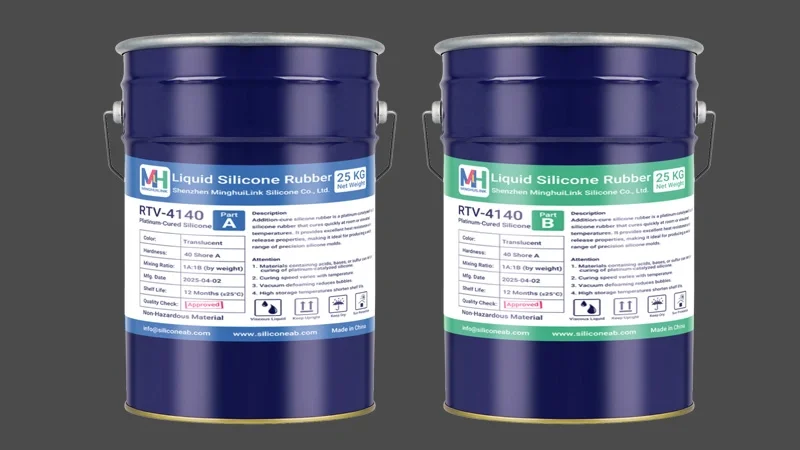
This series of High Hardness Platinum Cured Silicone Rubber, also known as Addition Cure Silicone, is a premium RTV-2 silicone material known for its excellent dimensional stability and high strength. It consists of Part A and Part B, which are supplied as translucent, viscous liquids.

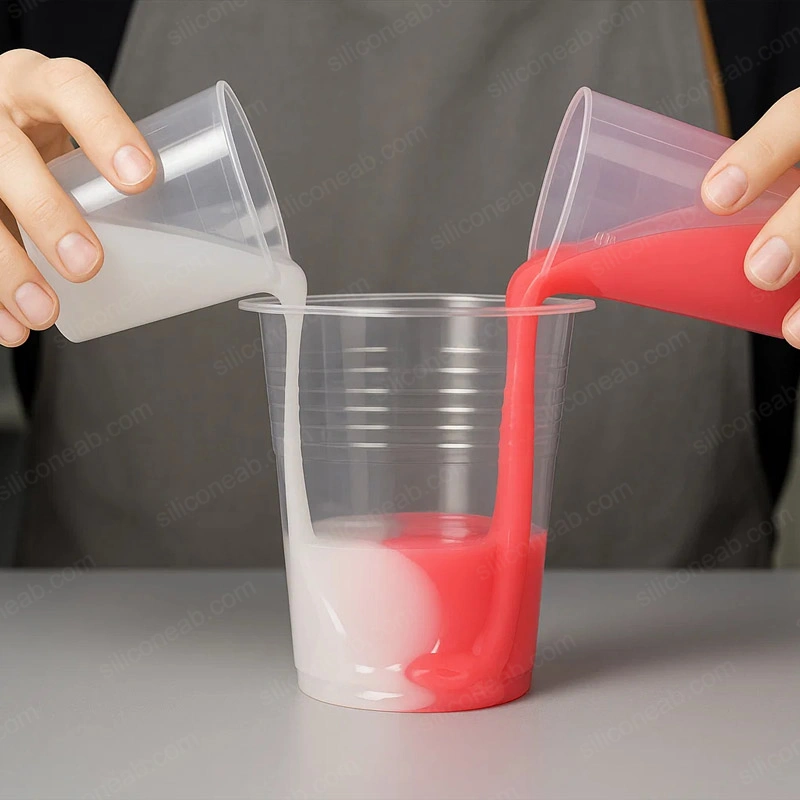
When mixed in a 1:1 ratio by weight, it cures to a rigid rubber at room temperature or can be accelerated with heat. It is the premier choice for creating robust, non-deforming molds used in rapid prototyping, composite manufacturing, and high-precision industrial casting.
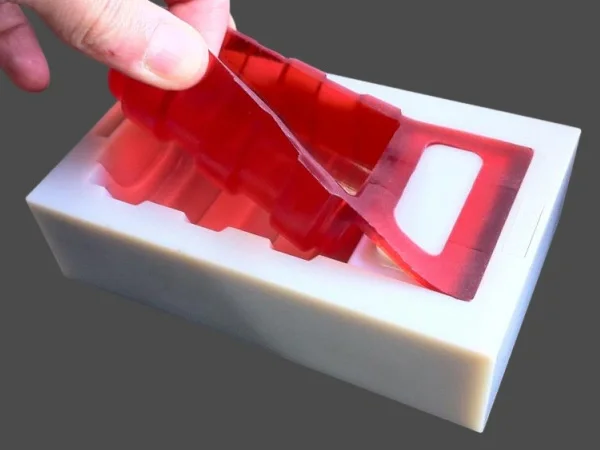
high hardness platinum cured silicone

2. Features

  • Easy Operation: Convenient 1:1 mix ratio by weight (recommended) or volume.
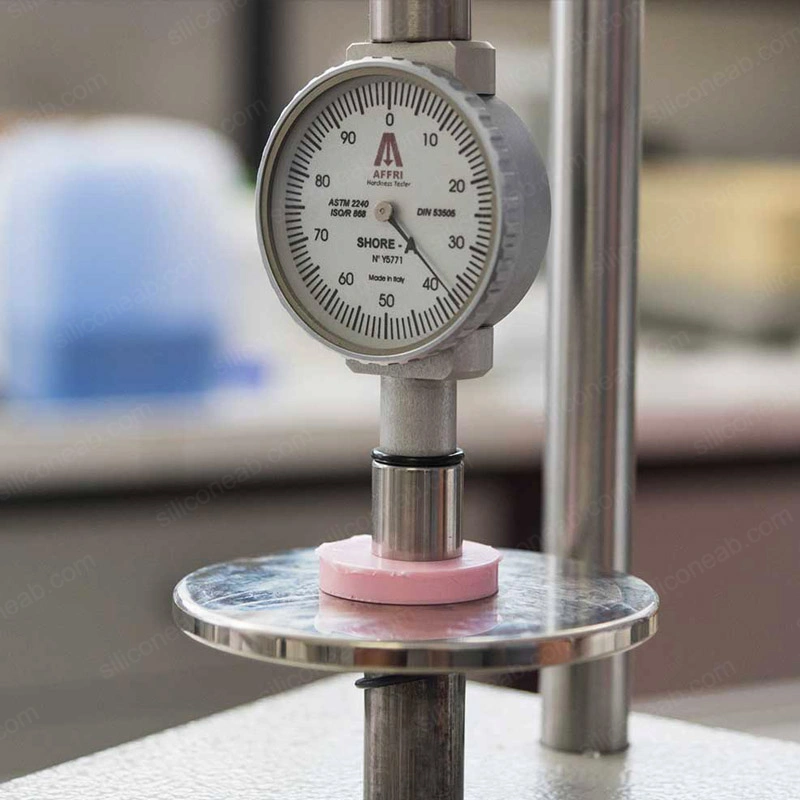
  • High Rigidity: High hardness (40-50 Shore A) ensures the mold maintains its shape under pressure.
  • Dimensional Stability: Excellent resistance to deformation, crucial for precision parts.
  • Ultra-Low Shrinkage: Minimal shrinkage (≤0.1%) ensures accurate reproduction of dimensions.
  • Clean & Safe: Platinum cure system produces no by-products; odorless and non-toxic.
  • Heat Resistance: Durable up to 250°C (482°F), suitable for high-exotherm resins.
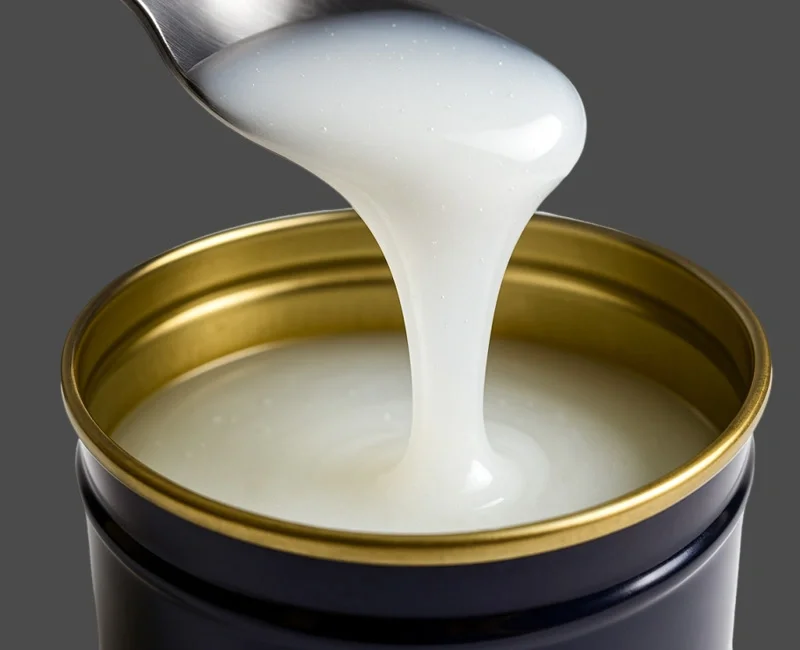
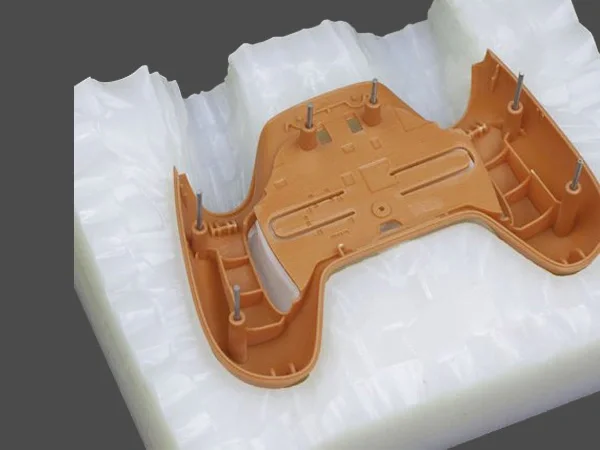
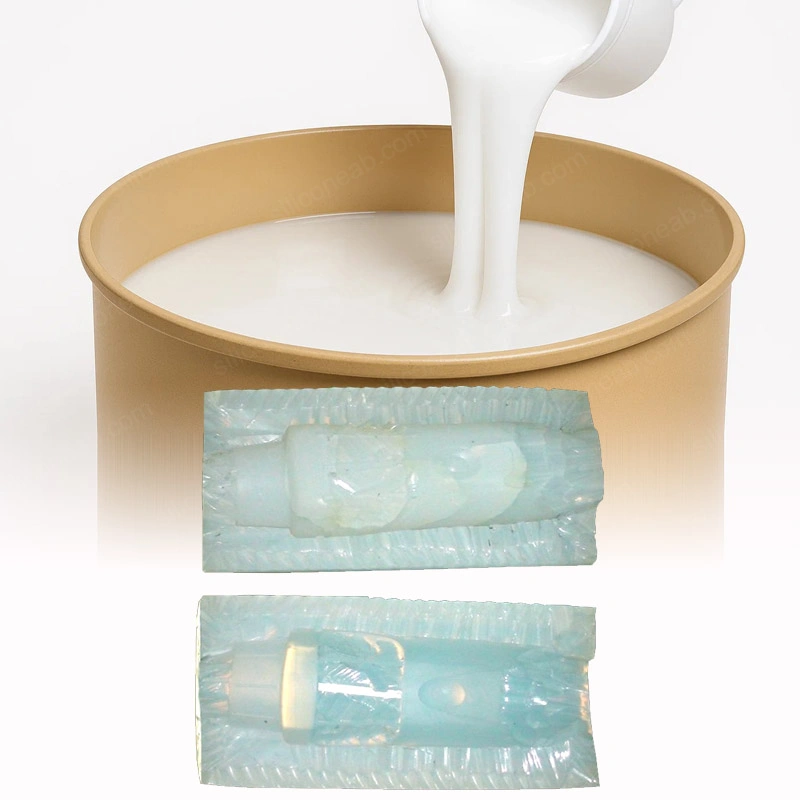
addition cure liquid silicone

3. Applications

This series is engineered for industrial applications where mold rigidity is paramount. It resists deformation during casting, making it ideal for:

  • Vacuum Casting (Rapid Prototyping): Creating precise silicone molds for small-batch production using PU resins (ABS-like, PC-like, Nylon-like). Its rigidity is crucial for casting thin-walled parts (e.g., electronic casings) without distortion.
  • Resin Casting: Ideal for casting epoxy resin, polyurethane (PU) resin, and polyester resin parts requiring high dimensional accuracy.
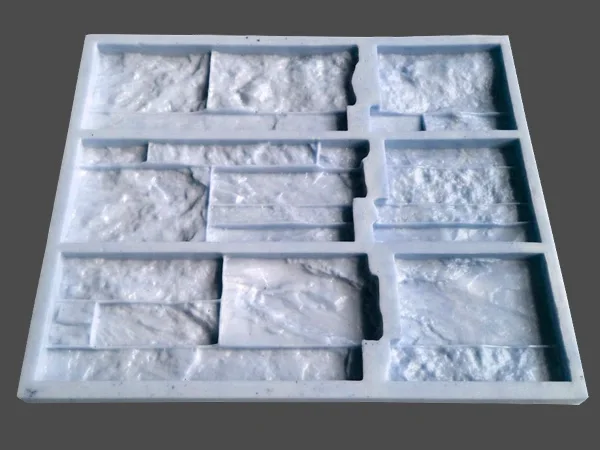
  • Construction & Decor: Creating rigid molds for heavy casting materials such as concrete, cement, and cultural stone bricks.
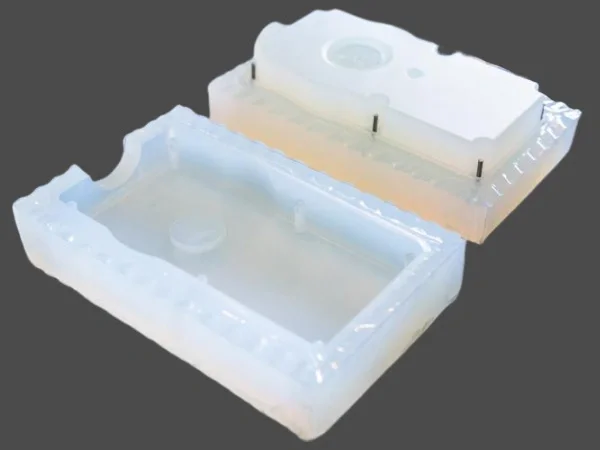
  • silicone rubber for rapid prototyping

    Rapid Prototyping

  • polyurethane rubber casting

    PU Rubber Casting

  • silicone rubber for thin shell casting

    Thin Shell Casting

  • concrete silicone mold

    Concrete/Brick Mold

4. Processing Notes

  1. Batch Consistency: Always use Part A and Part B from the same kit and batch. If mixing components from different batches, perform a small-scale test first to ensure compatibility.
  2. Compatibility Test: It is strongly recommended to conduct a small-scale test to confirm compatibility with your specific materials before starting a large project.
  3. Mixing Conditions: For optimal results, mix and cure between 20-30°C (68-86°F) with relative humidity below 50%.
  4. Temperature Limits: Do not use at temperatures below 15°C (60°F), as curing may be incomplete or significantly delayed.

Cure Inhibition Warning

The platinum catalyst is sensitive to contaminants. Ensure all tools and models are clean. Avoid contact with Sulfur (clays, latex gloves), Tin (condensation silicones), Amines (epoxy resins), and 3D Printed UV Resin (SLA/DLP), as these will prevent curing and leave a tacky surface.


Troubleshooting & Solutions:

5. Safety Precautions

Under normal storage and handling conditions, this product is stable and will not undergo hazardous reactions. However, standard industrial hygiene practices should be followed.

  • General: Keep out of reach of children.
  • Skin Contact: Wash thoroughly with soap and water.
  • Eye Contact: Rinse thoroughly with clean water for at least 15 minutes and seek medical attention.
  • Inhalation: Under normal conditions of intended use, this material is not considered an inhalation hazard.
  • Ingestion: Do not induce vomiting. Rinse mouth and seek medical attention.

6. Storage & Shelf Life

Storage Conditions
Store in a cool, dry place at room temperature (15-25°C / 60-77°F). Keep away from direct sunlight, acids, and bases.
Shelf Life
24 months from the date of manufacture when stored properly. High temperatures may reduce shelf life.
Opened Containers
Reseal immediately after use to prevent contamination and moisture ingress.
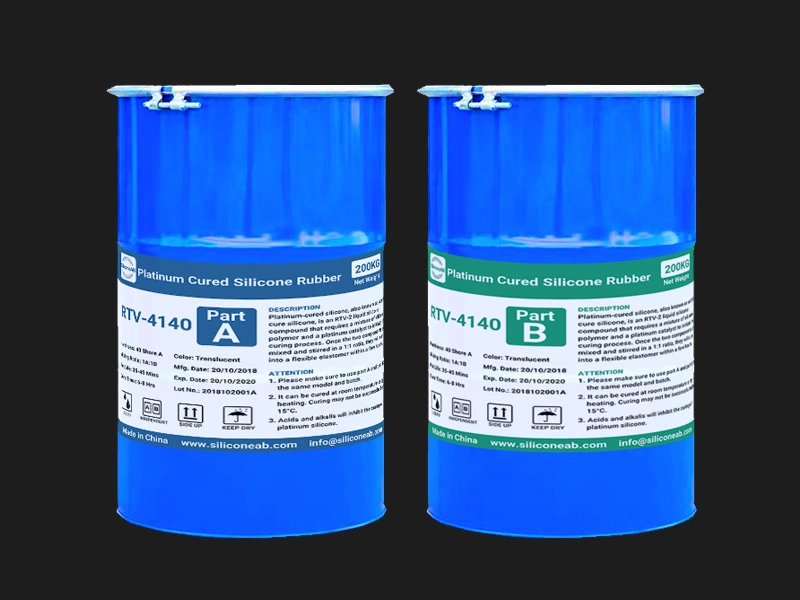
Beyond Shelf Life: If stored beyond the specified date, the product is not necessarily unusable. However, user testing is required to confirm performance before use.
Parameter Item Test Method RTV-4140 A/B RTV-4145 A/B RTV-4150 A/B
Unvulcanized Physical Properties @ 24 Hrs 25°C/77°F
Physical State - Liquid Liquid Liquid
Form - Viscous Viscous Viscous
Odor - Odorless Odorless Odorless
Part A Color ASTM E 1767 Translucent Translucent Translucent
Part B Color ASTM E 1767 Translucent Translucent Translucent
Part A Viscosity, mPa.s ASTM D 4287 4,800 8,500 7,000
Part B Viscosity, mPa.s ASTM D 4287 4,300 7,500 6,500
Specific Gravity, g/cm3 ASTM D 792 1.08-1.10 1.08-1.10 1.08-1.10
Part A and Part B mixed @ 25°C/77°F
Mix Ratio by Weight or Volume (A:B) - 1:1 1:1 1:1
Working Time, Minutes - 35 35 35
Curing Time, Hours - 6 6 6
Typical Properties of Cured Rubber @ 24 Hrs 25°C/77°F
Hardness, Shore A Durometer ASTM D 2240 40 45 50
Tear Strength, N/mm ASTM D 624 C 32.0 30.0 28.0
Tensile Strength, Mpa ASTM D 412 5.3 4.7 4.6
Elongation, % ASTM D 412 220 230 350
Shrinkage, % - ≤0.1 ≤0.1 ≤0.1
Heat Resistance, °C (°F) - 250 (482) 250 (482) 250 (482)

Step 1: Model Preparation

The master pattern should be thoroughly cleaned and dried. If the master pattern is fragile, weak, or porous, it may be necessary to apply a consolidant or sealant, and possibly fill in deep holes or crevices.

Step 2: Applying Release Agent

In most cases, a release agent is not necessary when using platinum-cure silicone. However, when the master pattern is highly porous, has a rough surface, numerous cracks or undercuts, or is otherwise difficult to demold, a thin layer of release agent may be recommended. The release agent should be compatible with both the platinum-cure silicone and the material of the master pattern.

For food-contact applications, make sure that the release agent is suitable for food-contact use and complies with the applicable regulatory requirements.

Step 3: Measuring & Mixing

Mix the desired amount of Parts A and B in a 1:1 ratio, preferably by weight, and thoroughly mix them together. Accurate measurement is essential to achieve the best physical properties of the cured platinum-cure silicone rubber.

If you wish to add color, use only a pigment or colorant that is compatible with platinum-cure silicone. Add a small amount and mix thoroughly until the color is uniform. For food-contact applications, use only colorants that are suitable for such applications.

Step 4: Vacuum Degassing

You can assess the need for vacuum degassing based on the specific requirements of each project, although vacuum degassing is recommended for achieving a high-quality, bubble-free finish. If vacuum degassing is used, place the mixed silicone in a container with a capacity of at least 3–4 times the volume of the material. Apply vacuum until the silicone rises and then collapses. Continue vacuuming until most of the air bubbles have disappeared, while taking care to prevent the silicone from overflowing.

Techniques to Reduce Air Bubbles:

  1. Hold the silicone container above the master pattern and allow the silicone to flow slowly in a thin stream. This helps break up air bubbles during pouring.
  2. Temporarily tilt the master pattern at an angle and pour the liquid silicone onto the higher end, allowing it to flow downward over the rest of the pattern. Once the silicone reaches the lower end, place the pattern flat and/or tilt or rotate it as necessary to achieve even coverage.

These techniques can be used alone or in combination. In addition, working at a lower temperature can extend the working time and allow more time for air bubbles to escape before curing. Do not alter the Parts A:B mixing ratio to control the working time or curing time.

Step 5: Pouring Silicone

Pour the silicone evenly, making sure that there is sufficient thickness above the highest point of the master pattern to provide the mold with the necessary mechanical strength. As a general guideline, a thickness of approximately 5 mm or more is recommended. However, the appropriate thickness depends on the size, geometry, and hardness of the mold.

Step 6: Demolding the Mold

Under normal conditions, platinum-cure silicone rubber cures at room temperature. At 25 °C (77 °F), the typical demolding time is approximately 4–6 hours. Higher temperatures can accelerate curing, while lower temperatures can increase the time required for the silicone to fully cure.

The actual demolding time may vary depending on the ambient temperature and working conditions. Before demolding, make sure that the silicone has fully cured and that the surface is dry and non-tacky. To achieve the specified final physical properties, a full cure of 24 hours at 25 °C (77 °F) is recommended.

  • Anon2024-10-08

    Can this be safely used to make pacifiers?

    Author Reply:Our product is RTV silicone, which is usually used for silicone mold making. Nipples are usually made with injection molding (LSR) silicone from the HTV silicone category.

  • Elijah2023-05-02

    Is it heat-resistant after being made into a mold with this food-grade liquid silicone? As in can I bake it at a low temp?

    Author Reply:Our silicone is a heat-resistant material, so it can be baked at low temperatures. In fact, silicone is often used in baking molds because it is non-stick and easy to clean.

  • Elma2023-04-30

    Could I add solid fine mesh powders to this product for coloring purposes?

    Author Reply:For optimal performance and successful curing of silicone, we highly recommend using specialized silicone pigments for coloring instead of adding any powders to the mixture. The addition of powders may weaken the overall performance of the silicone and affect its curing process. Furthermore, it's important to note that platinum-cured silicone can be sensitive to certain chemical elements, which may result in curing inhibition.

  • Ahern2023-04-23

    I've been trying to make molds out of 3D-printed UV resin masters lately, but the platinum-cure liquid silicone has been failing to cure. I've tried curing it at different temperatures and it still doesn't work.

    Author Reply:What material are your 3D-printed molds made of? Is the liquid silicone you're using cured in other situations, such as in disposable plastic cups? I recommend either baking the 3D-printed UV resin master at 60°C to evaporate potential solvents, or spraying the 3D-printed part with clear acrylic paint as a protective coating.

  • Beau2023-04-22

    Is it petrol resistant? To create a gasket for a carburetor?

    Author Reply:In my opinion it is not fit for purpose.

  • Aiden2023-04-16

    Is it compatible with 3D-printed objects with uv photopolymer resin?

    Author Reply:To use a 3D-printed object made of UV-sensitive resin as a master, it should be fully hardened before use by exposing it to sunlight or an artificial UV light source. Alternatively, you can spray a layer of primer on the UV-photosensitive resin master model. Otherwise, the silicone on the contact surface may be a little sticky.

Leave a Comment

Anonymity
verification code
More>>

Related Products